Industries / Banana Ripening
Banana Ripening Chamber Manufacturer in India for 4-Tier and 8-Tier Ripening Rooms
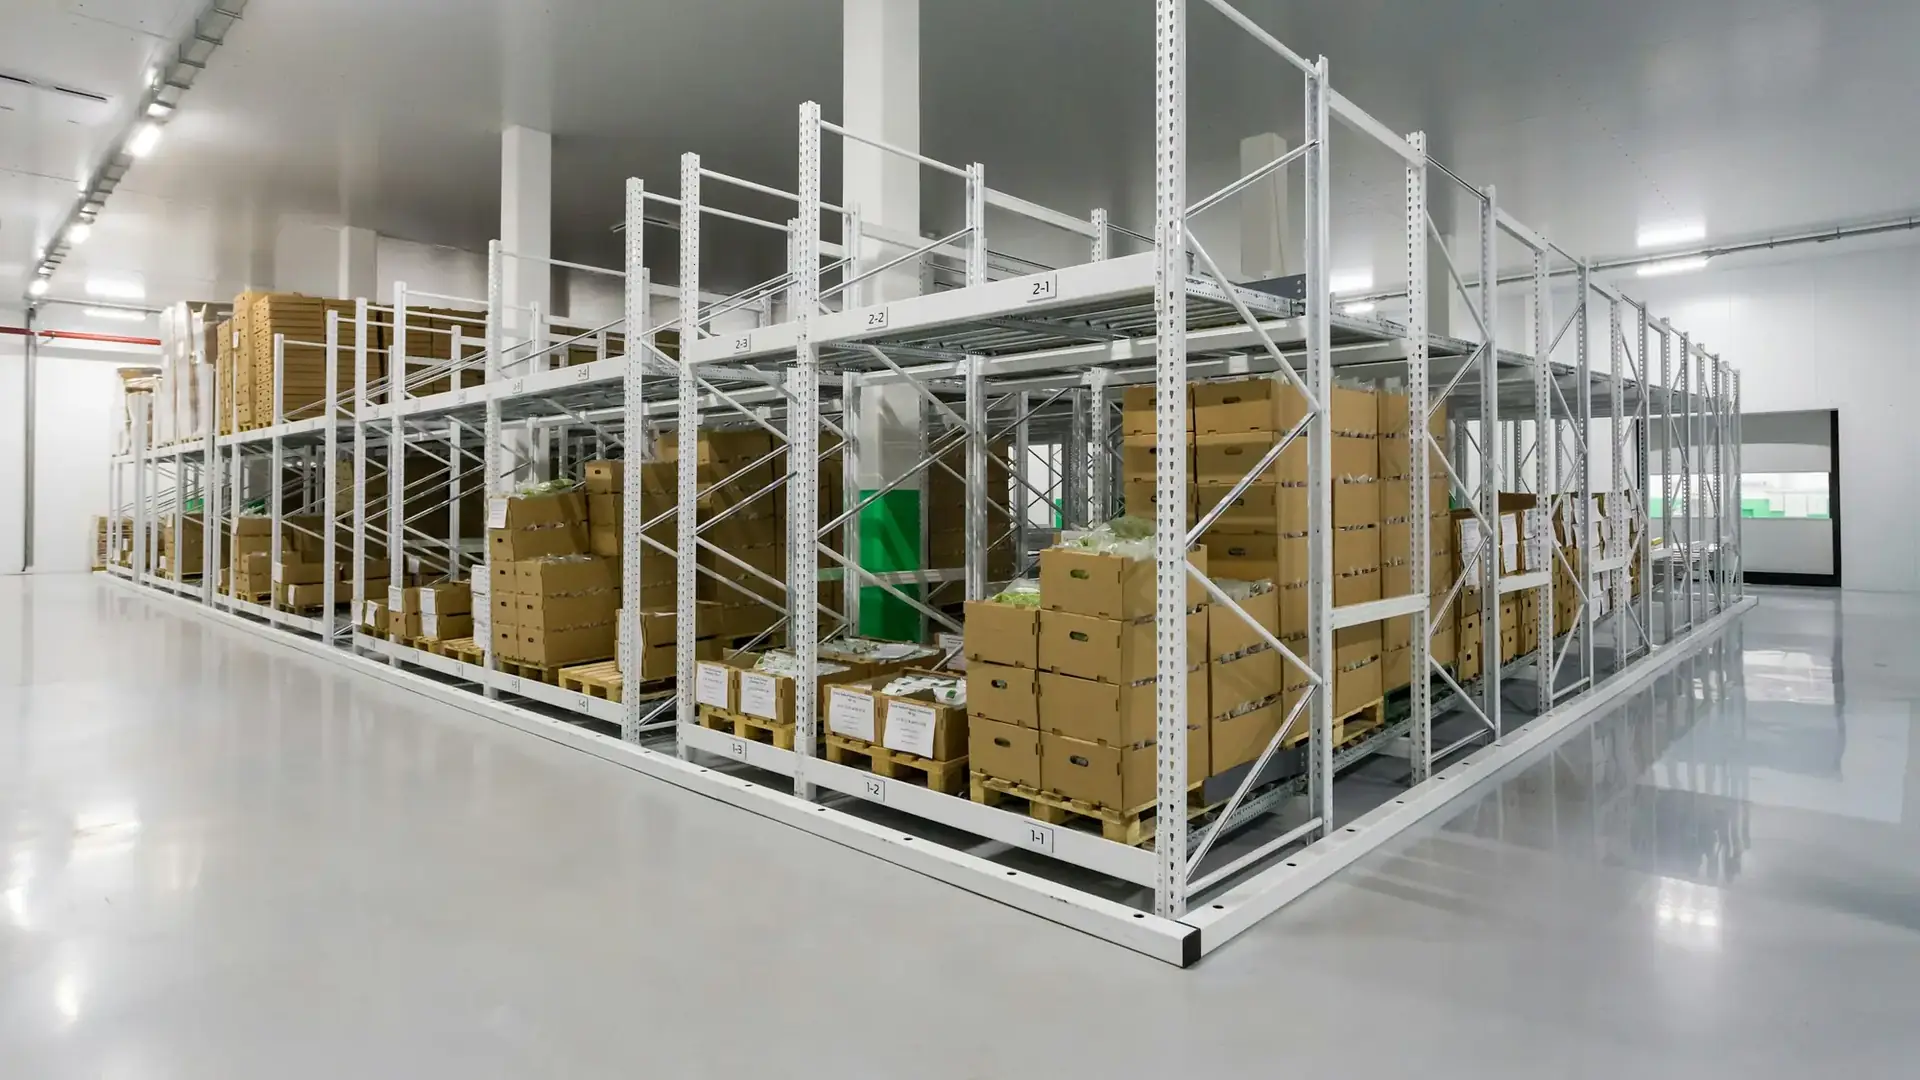
Modern banana ripening uses sealed ethylene chambers to ripen Cavendish bananas uniformly in 4–6 days instead of 10–14. HyperCold builds 4-tier and 8-tier banana ripening rooms with precise temperature, humidity, ethylene dosing and CO₂ scrubbing — eligible under NHB, MIDH and PMKSY ripening-chamber sub-schemes.
Capacity ranges from a single 12 MT chamber for a local distributor to multi-chamber 100+ MT central ripening units serving entire cities.
- Pressurised, gas-tight room with positive air-throw
- Ethylene dosing system with flow meter
- CO₂ scrubbing — fresh-air dampers + sensor
- Humidity holding 85–90% RH
- Temperature 14–18°C operating band
- Subsidy-eligible under NHB, MIDH, PMKSY
Typical applications
Operating Temperature
14°C – 18°C
Relative Humidity
85–90%
Engineering note
Ethylene 100–150 ppm, CO₂ kept below 1,000 ppm via scrubbing. Pressurised, gas-tight room.
Technical Specifications & Construction
Every banana ripening chamber we build follows the same engineering discipline — sized to your load, not picked off a brochure. Specifications below reflect typical HyperCold builds.
- PUF panel density
- 40 ± 2 kg/m³ (CFC-free polyurethane)
- Panel thickness (chiller)
- 80 mm or 100 mm
- Panel thickness (freezer)
- 125 mm or 150 mm
- Skin
- 0.5 mm PPGL / GI pre-coated steel both sides
- Joinery
- Cam-lock with EPDM gaskets
- Floor
- PUF + chequered Al / heated floor for freezers
- Refrigeration
- Daikin / Bitzer / Emerson scroll or screw
- Refrigerant
- R-404A / R-449A / R-507 as per BIS & MoEF norms
- Controls
- Carel / Danfoss digital with data-logger
- Door
- Hinged / sliding insulated + safety release
- Ethylene flow
- 5–10 ppm/hour metered dose
- CO₂ scrubbing
- Fresh-air damper with sensor feedback
- Air-throw
- 30–60 ACH, side-throw evaporators
- Capacity / chamber
- 12, 18, 24 or 32 MT per room
How HyperCold Designs This Cold Room
These are the design factors we lock down before quoting. Skip any of these and the project either runs hot, drinks electricity, or under-delivers on shelf life.
Product-specific temperature & humidity
We design from the commodity's psychrometric envelope, not a generic chiller spec. Different storage life targets get different design points.
Humidity & moisture control
Coil sizing, defrost strategy and air-throw decide whether your product dries out, sweats, or holds quality.
Air change rate & throw pattern
Velocity through the stack governs uniform pull-down. We engineer 25–60 ACH per room volume, not a default.
Refrigeration sizing on actual load
Heat load is calculated from product, infiltration, lighting, defrost, motor and personnel — never a TR/MT thumb rule.
Panel selection by ambient
100 mm in moderate zones, 150 mm in Rajasthan / interior MH. Panel density never below 40 kg/m³.
Serviceable layout & AMC access
Compressor decks, drain lines and electrical panels laid out for one-hand servicing — saves cost over 10 years.
What Drives the Project Cost
We don't quote square-foot rates — every build is BOQ-priced. The factors below decide where your project lands within a realistic range.
- 01Internal volume in CFT and storage tonnage
- 02Target temperature band (chiller, freezer, sub-zero, deep-freeze)
- 03PUF panel thickness and density
- 04Refrigeration capacity (TR) and compressor brand
- 05Daily product load and door-opening frequency
- 06Insulation upgrades for Tier-2 / hot-climate sites
- 07Civil work, levelling, drainage and trenching
- 08Electrical infrastructure, DG backup and stabilisation
- 09Automation level — basic, IoT-enabled, or SCADA
- 10Installation distance from Sirsaganj base and site access
- 11GST and statutory inclusions (toggled in BOQ)
- 12AMC tier — Standard, Pro, or 24×7 Critical
Why Operators Choose HyperCold
Uniform ripening
Side-throw fans and pallet-stack design ensure every box of every tier ripens at the same rate.
Gas-tight construction
Special door gaskets and panel jointing keep ethylene inside and CO₂ scrubbing effective.
Subsidy-ready
Bankable DPR for NHB Cap A, MIDH and PMKSY ripening-chamber schemes.
Energy-aware design
Heating + cooling sized correctly so the chamber doesn't fight itself — 30–45% lower kWh vs poorly sized rooms.
Frequently Asked Questions
Subsidies & finance that may apply
Eligibility depends on project type, applicant category, state and current government notification. Below is indicative — verify with the official scheme portal before applying.
MIDH (State Horticulture Mission)
Credit-linked back-ended capital assistance for horticulture cold storage and pack houses.
Read scheme detailsNHB Cold Storage Subsidy
National Horticulture Board capital subsidy for cold storage and CA storage projects.
Read scheme detailsMoFPI Integrated Cold Chain (PMKSY)
Grant-in-aid for integrated pre-cooling, IQF, blast freezing, CA and reefer logistics.
Read scheme detailsAgriculture Infrastructure Fund (AIF)
Interest subvention and credit guarantee on bank term loans for post-harvest infrastructure.
Read scheme detailsPMFME — Micro Food Processing
Credit-linked subsidy for micro food processing units including small cold rooms.
Read scheme detailsState Subsidy Schemes
State Horticulture, Food Processing, SC/ST and SHG components vary by state action plan.
Read scheme detailsMSME & Bank Finance (CGTMSE, SIDBI, NABARD)
Term loan and working capital options via scheduled banks, SIDBI, NABARD and cooperatives.
Read scheme detailsReady to scope your banana ripening chamber?
Share your product, room size, and target temperature. We'll send a BOQ-priced quote with PUF, refrigeration, installation, and AMC — pan-India delivery from Sirsaganj, Firozabad.